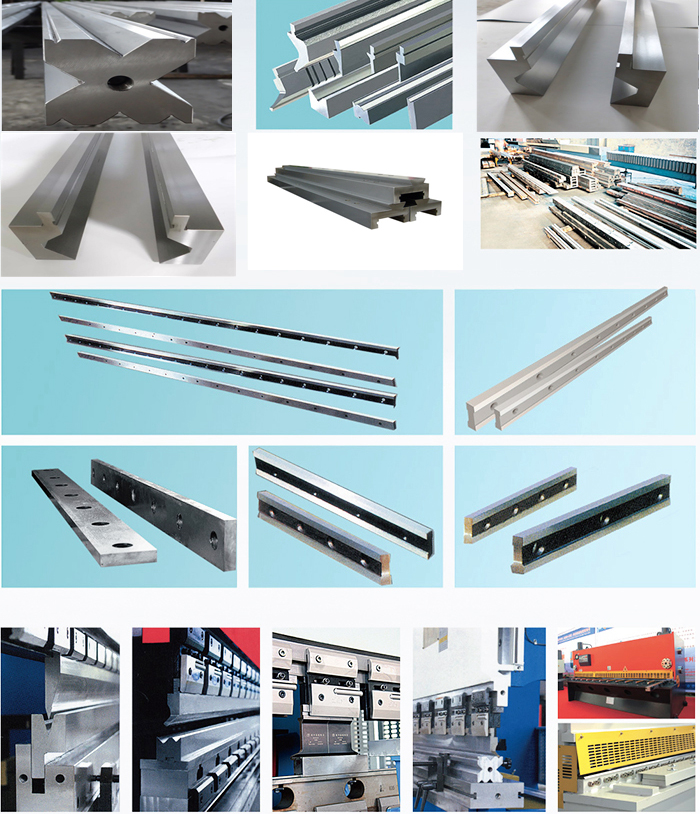
Shearing machine blades – Bending machine tooling
Shear blade materials: 9CrSi, 6CrW2Si, Cr12MoV, H13, LD, SKD-11, D2, 1.2344, HM-1.
Hardness after quenching: HRC 50°–63°
Tolerance: ±0.002
Blade specifications: Standard shear blades available from stock. Non-standard blades can be custom manufactured according to customer drawings and requirements.
Other services: Blade grinding, resharpening, repair, and maintenance.
Shear blades are applicable to: various types of profile shears, bar shears, plate shears, and other shearing equipment. Products include blades for hydraulic shears, bar shearing machines, profile plate shears, high-precision CNC shears, and more.
Shear Blade Gap Adjustment
First, adjust the gap between the upper and lower blades to 0.5 mm, then use a feeler gauge to adjust from one end to the other, ensuring the gap is consistent across the entire blade length. Then return the blade edge to zero clearance.
Next, perform fine adjustments (carefully observe during operation to avoid the upper and lower blades contacting each other). At the zero position, a 0.03 mm feeler gauge should pass through, while a 0.05 mm gauge should not.
Adjust the gap appropriately to approximately 1/10 to 1/20 of the sheet thickness being cut.
If the blades are sharp but the cut sheet edges show burrs, the gap between the upper and lower blades can be slightly reduced.
Shear Safety Operating Procedures
1. The shear must be operated and maintained by designated personnel. Operators must be familiar with the machine's structure and performance.
2. Overloading the shear is strictly prohibited. Do not cut hardened steel, hard alloy steel, high-speed steel, alloy steel, castings, or non-metallic hard materials.
3. Shear blades must be kept sharp. Dull or damaged blades should be ground or replaced promptly.
4. When multiple operators are working, one person must be designated to coordinate and direct the operation.
5. Do not cut two different materials of different specifications simultaneously on the shear, nor cut multiple layers stacked together.
6. When feeding material, keep hands away from the gap between the sheet and the worktable. When cutting short pieces, use a steel plate to hold them down. Fingers must be at least 200 mm away from the blade edge during cutting.
7. After aligning the sheet with a pry bar, remove the pry bar immediately before cutting. If the sheet shifts, secure it with wooden blocks to prevent the pry bar from springing out and causing injury when the hold-down foot descends.
8. Cut workpieces must be placed stably and not stacked too high. Trim scrap and waste should be cleared promptly to keep the work area clean.